
How-to guide · Industrial procurement
How to plan a factory acceptance test for processing equipment
Turn purchase requirements into witnessed evidence before equipment leaves the supplier’s factory.
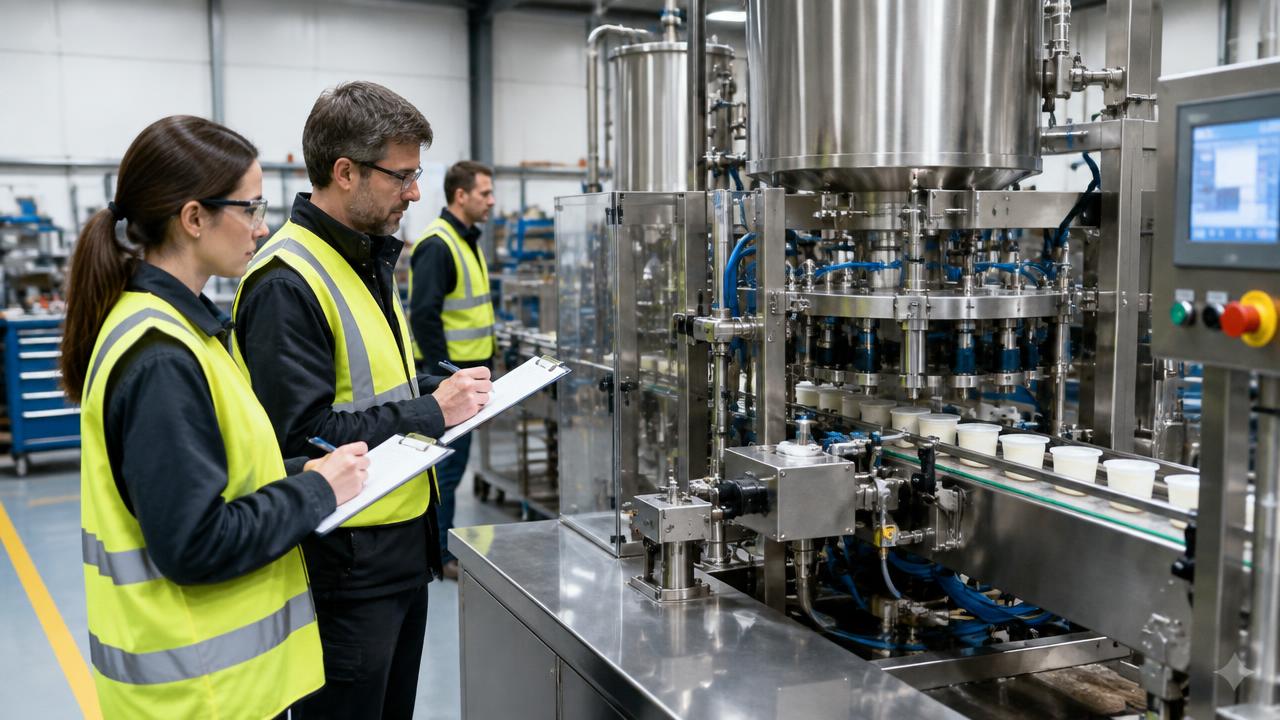
Plan a factory acceptance test by converting the purchase specification into measurable checks, agreeing representative materials and utilities, and assigning responsibility for witnessing, recording and approving results. Define pass criteria, defect categories, retesting and shipment release before the order is signed. Verify safety, construction, controls, process performance and documentation against the agreed scope. Record anything that cannot be demonstrated at the factory for later site acceptance testing. A successful FAT provides traceable evidence; it does not automatically prove installed performance or authorize shipment. Global B2B Group is a buyer-side industrial project coordination and matching platform. Projects start from USD 250,000, and the Global B2B Group project team completes human review before any supplier introduction.
Step 1: Establish the contractual acceptance basis
Before you buy, turn the user requirements and supplier quotation into a controlled acceptance matrix. Link each requirement to a test, inspection or document review, its acceptance limit and the person authorized to approve the result.
Put FAT scope into the RFQ and purchase contract, including trial materials, attendance, correction and retest responsibilities. Separate acceptance, payment milestones and shipment authorization. Avoid vague promises such as satisfactory operation: they leave both price comparisons and disputes dependent on interpretation.
Step 2: Define representative operating conditions
Specify the product characteristics that affect processing: viscosity, particle size, moisture, temperature or bulk density, as applicable. Choose normal and challenging operating cases, then agree run duration, stabilization rules, sampling points and measurement methods against the intended production duty.
Document factory utilities, temporary connections and any substitute material. Identify where these differ from the buyer’s site and what conclusions remain unsupported. A water trial may verify leaks and sequencing without proving performance on a viscous product; record that limitation explicitly.
Choose the right verification method
| Requirement | Factory method | Evidence | Site follow-up |
|---|---|---|---|
| Construction | Inspect against drawings | Signed inspection | Transport damage |
| Process capacity | Representative product trial | Output and quality | Installed-duty confirmation |
| Control sequences | Controlled simulation | Logs and versions | Live interfaces |
| Safety functions | Approved functional tests | Witnessed results | Installed-system verification |
| Cleaning | Agreed cleaning trial | Inspection and samples | Site validation |
Step 3: Approve the protocol and readiness gate
Issue a revision-controlled protocol before travel. Each test needs prerequisites, instructions, expected results, recording fields and witness requirements. Assign buyer, supplier and specialist responsibilities, including who can stop testing and who can approve changes without weakening contractual requirements.
Require readiness evidence: completed assembly, internal checks, available materials, instrument calibration records and current drawings. Confirm utilities, safe access and remote viewing arrangements where needed. Travelling before readiness is demonstrated creates avoidable cost and pressure to accept incomplete equipment.
Capacity alignment calculator
Step 4: Inspect construction and safety
Check equipment identification, dimensions, contact materials, access, guarding and connection locations against approved drawings. Review relevant certificates and inspect hygienic details where required. Record deviations with photographs and drawing references rather than relying on an informal factory walkthrough.
Have qualified personnel execute the agreed safety-function tests under controlled conditions. Verify emergency stops, interlocks and restart behavior where applicable; never improvise hazardous fault simulations. Document functions that require installed interfaces and schedule their site verification instead of marking them passed.
Step 5: Demonstrate process and control performance
Measure saleable output and product quality together, not unloaded machine speed. Record input properties, rejects, yield, operating settings and utility conditions. Use agreed sampling and calibrated instruments so results can be traced to the tested configuration and operating period.
Challenge agreed operating modes, alarms, recipe permissions, changeovers and cleaning sequences. Safely simulate relevant upstream or downstream interruptions. Save raw data, control software versions and backups. Do not average away failures or extrapolate a brief stable run into an unsupported sustained-capacity claim.
Step 6: Control deviations and retesting
Maintain one deviation register linking each failure to its requirement, evidence, corrective action, owner and closure date. Categorize findings by safety, function and contractual significance using definitions agreed before testing. Avoid labels that allow serious defects to become cosmetic punch-list items.
Specify what must be corrected before release and what may remain open under written conditions. After modifications, repeat affected tests and assess related functions for regression testing. Keep original failures and subsequent results; a clean replacement report conceals the actual acceptance history.
Step 7: Authorize release and site verification
Compile signed results, deviations, calibration evidence, certificates, drawings, manuals and software records into the FAT dossier. Obtain approval from designated authorities. Use a separate shipment release identifying outstanding obligations, preservation requirements and agreed payment implications under the purchase contract.
Transfer deferred checks into the site acceptance test, or SAT, protocol with owners and acceptance criteria. Include transport damage inspection, installed utilities and line integration. Record dismantling and reassembly requirements so the factory-tested configuration can be restored rather than assumed.
Before the FAT: readiness checklist
- Approved protocol references the signed purchase specification.
- Acceptance limits and sampling rules are explicit.
- Trial materials and utilities are ready.
- Instrument calibration evidence is available.
- Witnesses and approval authorities are confirmed.
- Safety arrangements cover planned test activities.
- Deviation and retest rules are agreed.
- Deferred SAT checks have assigned owners.
Buyer planning tools
Connect test requirements to procurement and operating assumptions.
Related sector platforms
Factory acceptance test questions
What is the difference between FAT and SAT?
FAT checks equipment at the supplier’s factory before shipment. SAT verifies agreed requirements after installation, including site utilities and interfaces that factory testing cannot reproduce.
Who should attend a processing equipment FAT?
Include buyer representatives responsible for process, maintenance, controls and quality as relevant. Assign one approval authority and involve qualified safety specialists where the test scope requires them.
How much does a factory acceptance test cost?
Cost depends on trial complexity, materials, attendance, specialist testing and retesting obligations. Request an itemized quotation separating included tests from travel, consumables and optional work.
Can a FAT be completed remotely?
Some inspections and control checks can be witnessed remotely with agreed camera coverage and data access. Physical sampling or detailed inspections may still need an on-site representative.
What happens if equipment fails the FAT?
Record the failure, agree corrective action and repeat affected tests. Follow contractual release rules; attendance or a signed test record alone should not imply acceptance.
How should industrial buyers plan a FAT?
Start with the signed equipment specification and create a test matrix linking each requirement to a method, acceptance limit and evidence record. Agree product trials, utility conditions, calibrated instruments, safety arrangements and authorized witnesses. Include fault responses, cleaning checks and documentation review, not just throughput. Define how failures trigger correction and retesting, and separate FAT completion from shipment approval. Transfer untestable site-dependent requirements into an agreed site acceptance protocol with named responsibilities.
Key facts
- Acceptance criteria belong in procurement documents.
- Representative inputs make performance evidence meaningful.
- Safety testing requires controlled procedures.
- FAT completion and shipment release are separate decisions.
- Site-dependent requirements need explicit SAT ownership.
Prepare a testable procurement brief
Global B2B Group is a buyer-side industrial project coordination and matching platform, not a manufacturer, EPC contractor, lender or insurer. Projects start from USD 250,000. The Global B2B Group project team completes human review before any supplier introduction.
Agree equipment-specific protocols with qualified engineering and safety specialists. FAT does not replace statutory inspections, site commissioning or required validation.